
AWG measures conductor diameter, mm² measures cross-sectional area, so the two never convert exactly. Here is how to read both systems and match a terminal barrel to the conductor.
AWG defines a conductor by diameter; mm² defines it by cross-sectional area. The two systems were standardised independently, so an exact conversion always lands between the metric sizes — which is why a terminal should be chosen by its published wire range, not by the number printed on the wire.
Terminal drawings circulate in both systems, and a single project can carry both at once: equipment designed in North America arrives with AWG specifications, while the cable and the terminal barrel are ordered in mm². The numbers look interchangeable, and they are not. This guide explains what each system actually measures, gives the conversion table that matters for terminals, covers the conductor classes that decide whether a barrel will close, and ends with a check you can apply before placing an order.
AWG, the American Wire Gauge, describes the diameter of a solid round conductor on a logarithmic scale. The scale runs backwards: a larger AWG number means a thinner conductor, and every six gauge steps the cross-sectional area halves. Moving from 18 AWG to 12 AWG is roughly a fourfold increase in area, not a doubling — a point that matters when a drawing moves several gauges at once.
The metric system describes the conductor’s cross-sectional area directly, in square millimetres. IEC 60228 fixes the standard sizes used across Europe, Asia and much of the rest of the world: 0.5, 0.75, 1, 1.5, 2.5, 4, 6, 10, 16, 25, 35, 50, 70, 95, 120 mm² and upward. A cable is ordered as “2.5 mm²” because that is the nominal area the standard specifies.
Because one system defines a diameter and the other an area, converting between them produces values that fall between the metric sizes. 16 AWG has an actual area of 1.31 mm², close to 1.5 mm² but not equal to it. 14 AWG is 2.08 mm², and not 2.0 mm², because 2.0 mm² does not exist in the IEC 60228 sequence at all. Figure 1 shows the same conductor measured both ways: one number reads across the wire, the other counts what fills it.
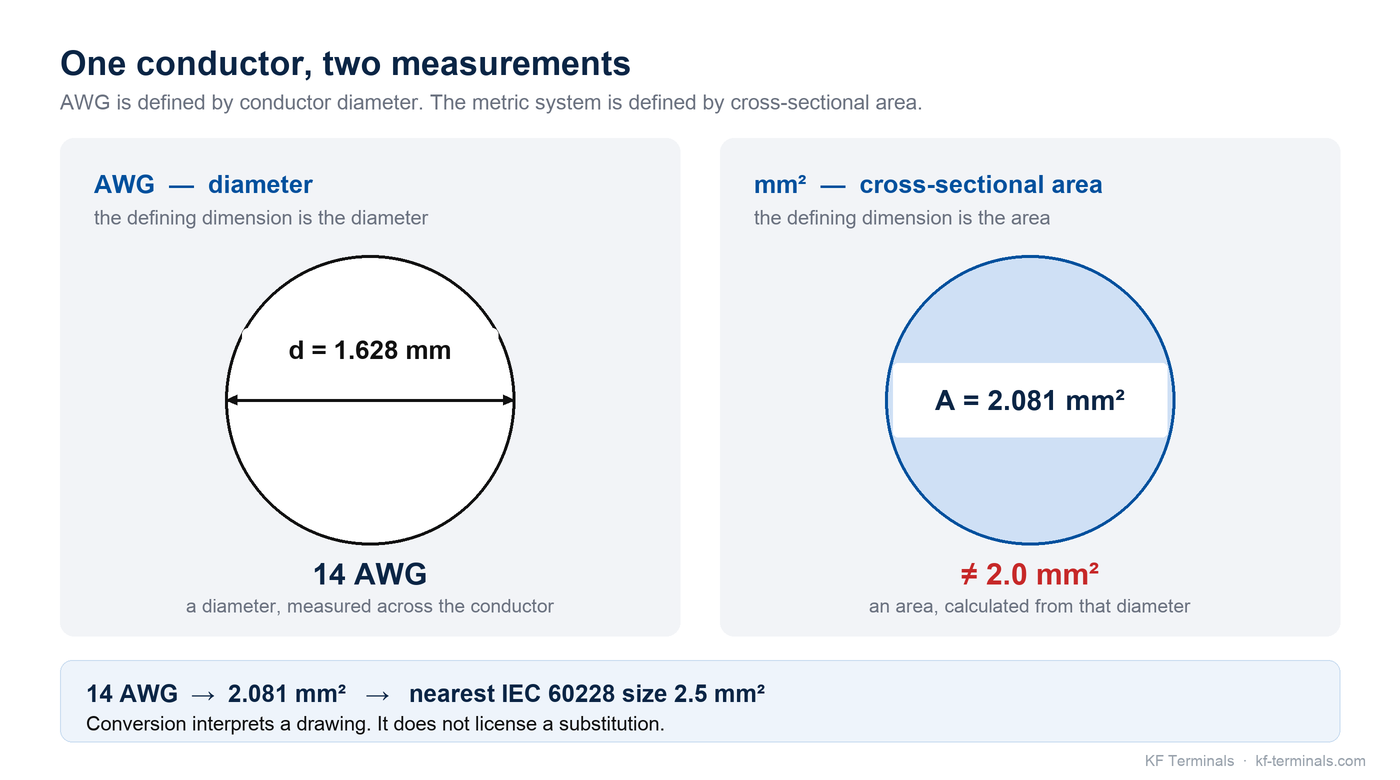
Figure 1 — The same 14 AWG conductor, measured both ways. AWG fixes a diameter of 1.628 mm; the area that results is 2.081 mm², which sits between the 1.5 and 2.5 mm² standard sizes. There is no 2.0 mm² step to round to.
Conversion is a tool for reading a drawing; it is not a licence to substitute one size for another.
The table below covers the range used most often in control panels, harness work and industrial wiring. Diameters and areas are calculated from the AWG defining formula, and the right-hand column gives the nearest IEC 60228 standard cross-section for reference.
| AWG | Diameter (mm) | Actual area (mm²) | Nearest IEC 60228 size |
|---|---|---|---|
| 20 | 0.812 | 0.518 | 0.5 |
| 18 | 1.024 | 0.823 | 0.75 |
| 17 | 1.151 | 1.040 | 1.0 |
| 16 | 1.291 | 1.309 | 1.5 |
| 15 | 1.450 | 1.650 | 1.5 |
| 14 | 1.628 | 2.081 | 2.5 |
| 13 | 1.828 | 2.624 | 2.5 |
| 12 | 2.053 | 3.309 | 4 |
| 11 | 2.305 | 4.172 | 4 |
| 10 | 2.588 | 5.261 | 6 |
| 8 | 3.264 | 8.367 | 10 |
| 6 | 4.115 | 13.30 | 16 |
| 4 | 5.189 | 21.15 | 25 |
| 2 | 6.544 | 33.63 | 35 |
| 1 | 7.348 | 42.41 | 50 |
| 1/0 | 8.252 | 53.49 | 50 |
| 2/0 | 9.266 | 67.43 | 70 |
| 3/0 | 10.40 | 85.03 | 95 |
| 4/0 | 11.68 | 107.2 | 120 |
Read the table with three cautions in mind.
First, the nearest-size column is a convenience for interpretation, not an instruction. 18 AWG measures 0.823 mm² and sits between the 0.75 and 1.0 mm² standard sizes; which one a terminal accepts depends on the terminal, not on which number happens to be closer.
Second, the gap widens as the conductor grows. 4/0 AWG is 107.2 mm² and the nearest IEC size is 120 mm² — a difference of about 12%, which matters when a lug is specified by area rather than by gauge.
Third, some pairings in common use are approximations that work for a different reason. 1 AWG is frequently written against 50 mm² and 2 AWG against 35 mm², but the actual areas are 42.4 mm² and 33.6 mm². The pairing is practical because terminal ranges overlap; it is not evidence that the two sizes are equal, and it should not be adopted as a conversion rule.
A conductor’s cross-section is only half its specification. IEC 60228 also defines the conductor class: Class 1 is a single solid wire, Class 2 is stranded for fixed installation, Class 5 is flexible, and Class 6 is extra-flexible, intended for continuous movement in cable chains and on moving machinery.
Two cables both marked 2.5 mm² can therefore be built from completely different strands. At 2.5 mm² the standard stranding tables give 1 × 1.78 mm for Class 1, 7 × 0.67 mm for Class 2, and roughly 50 × 0.26 mm for Class 5 against 140 × 0.16 mm for Class 6. Classes 1 and 2 fix the strand count; classes 5 and 6 fix the maximum strand diameter and the conductor resistance, which is why published tables differ slightly around the same nominal area. The copper area is the same in all four cases; the construction is not, as Figure 2 shows.
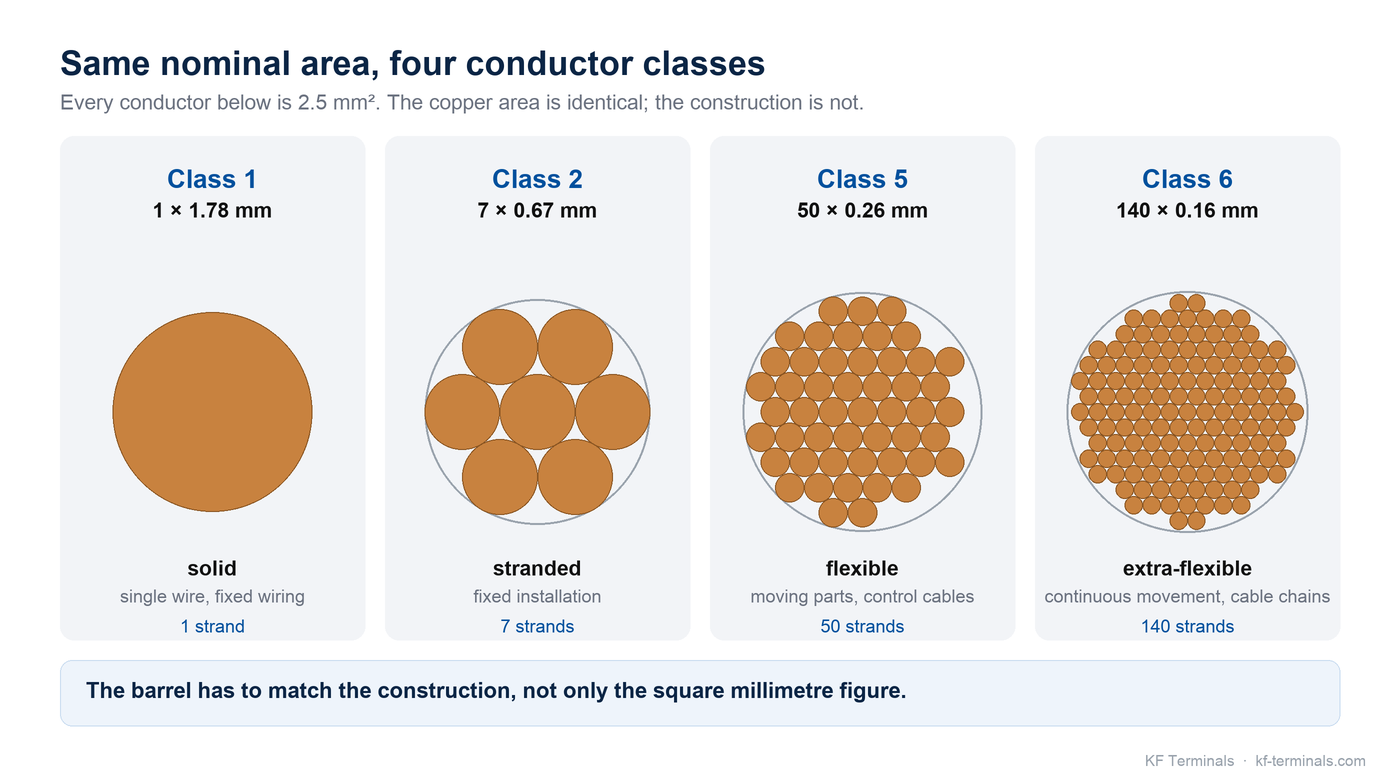
Figure 2 — Four conductors, one nominal area. All are 2.5 mm², drawn to a common scale. The class decides the strand construction, and the strand construction is what the barrel has to close around — which is why a square millimetre figure alone does not settle the choice of terminal.
That difference is modest in the cross-section and decisive at the crimp. A barrel sized for a solid conductor may not close correctly around a fine-strand conductor of the same nominal area, and the two are not interchangeable for that reason.
This is why the flexible end of the market uses its own product family. Cord end ferrules, also called wire end sleeves, are designed for Class 5 and Class 6 conductors, with a thin wall and a plastic collar that marks the size. Non-insulated terminals and copper tubular lugs are typically specified for Class 2 stranded conductors and for larger sizes. Where a project mixes classes — a flexible control cable landing on a terminal block, for example — the terminal’s published range and the conductor class both have to be checked, not just the square millimetre figure — see how cord end terminals keep fine strands together for the flexible case.
Mixed-system work is the normal case in export manufacturing, and it concentrates in a few familiar places.
Equipment designed in North America arrives with AWG schedules on the nameplate and in the wiring diagram, while the cable drums and the terminal stock in the factory are ordered in mm². The designer’s schematic and the buyer’s purchase order describe the same conductor in two different languages.
Automotive and harness work runs on both. Harness drawings are frequently issued in mm² for the cable and in AWG for connectors carried over from an existing platform, so the two appear on the same sheet and have to reconcile at the terminal — see joining conductors of different gauges for the splicing case.
Distribution and control panels are usually specified in mm², and the larger circuits land on copper tubular lugs that may be catalogued by AWG — the same physical lug can appear under either label depending on which market the catalogue was printed for.
Renewable and energy-storage installations are specified almost entirely in mm² at large cross-sections, where AWG notation is rarely used at all. The practical rule in every one of these cases is the same: settle which system governs the drawing, convert everything else into it, and confirm the final size against the terminal’s published range rather than against a conversion table alone.
Every terminal datasheet states a wire range — the smallest and largest conductors the barrel will accept. That range is the capacity window, and the conductor has to land inside it. Figure 3 shows the same conductor against a window that contains it and two that do not.
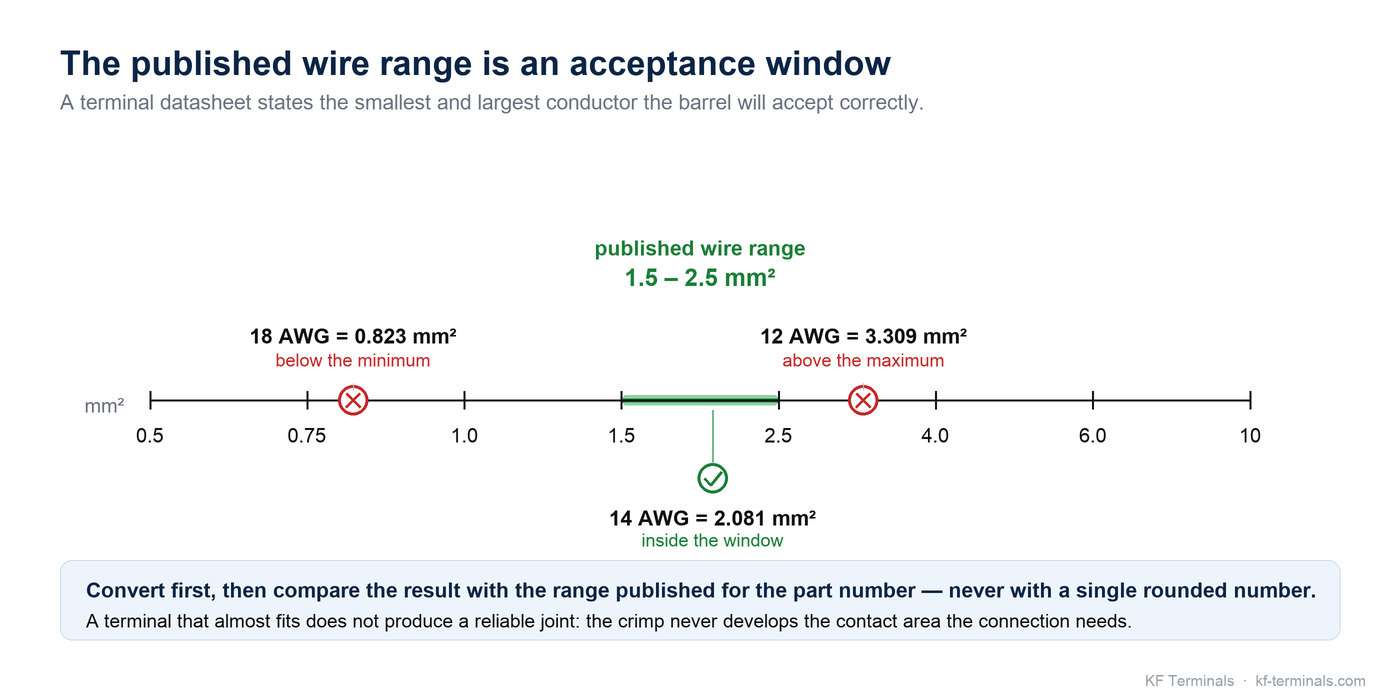
Figure 3 — A published wire range read as an acceptance window. 14 AWG falls inside a 1.5–2.5 mm² range at 2.081 mm²; 18 AWG is below the minimum and 12 AWG above the maximum. Convert the conductor first, then compare it with the range — never with a single rounded number.
Take the KF Type AWG copper tubular lug range, shown in Figure 4, as a working example. It covers AWG 8 through AWG 4/0, with stud sizes from #10 to 1/2 inch (5.1 mm to 13.1 mm), and it is specified for use with the OPT TP-150D and TP-150 crimping tools, depending on size. A drawing that arrives in AWG can be matched to this range directly, because the range is published in AWG. A drawing that arrives in mm² has to be converted first, and the converted value then compared with the range rather than with a single number on a catalogue page.
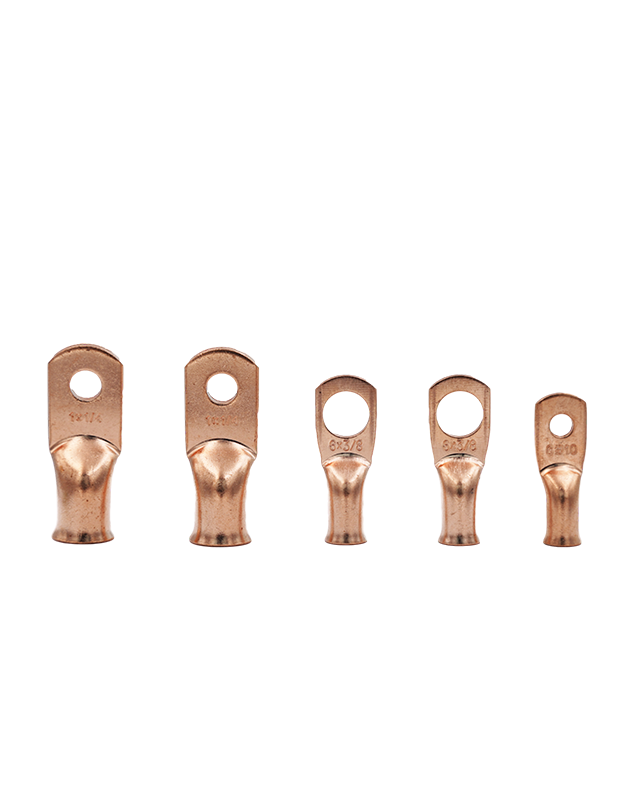
Figure 4 — KF Type AWG copper tubular lugs. Each conductor size in the range is a separate part number with its own set of stud sizes and its own recommended crimping tool, which is why the wire range is quoted across the family rather than as one figure.
Three steps cover most cases:
If the conductor sits between two published sizes, choose the terminal whose range contains it. Never round a conductor down to fit a smaller barrel: the crimp will not develop the contact area the joint needs, and a joint that passes a pull test can still run warm in service.
Most connection problems that reach a supplier as a quality complaint were decided at the ordering stage. These eight come up repeatedly.
Colour is the most visible feature of an insulated terminal and the least reliable way to select one. There is no single international colour map. Manufacturers and regional conventions differ, and a blue terminal from one factory may accept a different conductor range than a blue terminal from another.
The two terminals in Figure 5 come from the same manufacturer and carry the same vinyl insulation, and they differ in two ways that are not connected: one is a ring, the other a spade, and the collars are coloured differently. Colour tracks the conductor range. It does not describe the shape of the terminal, and it does not travel between brands.
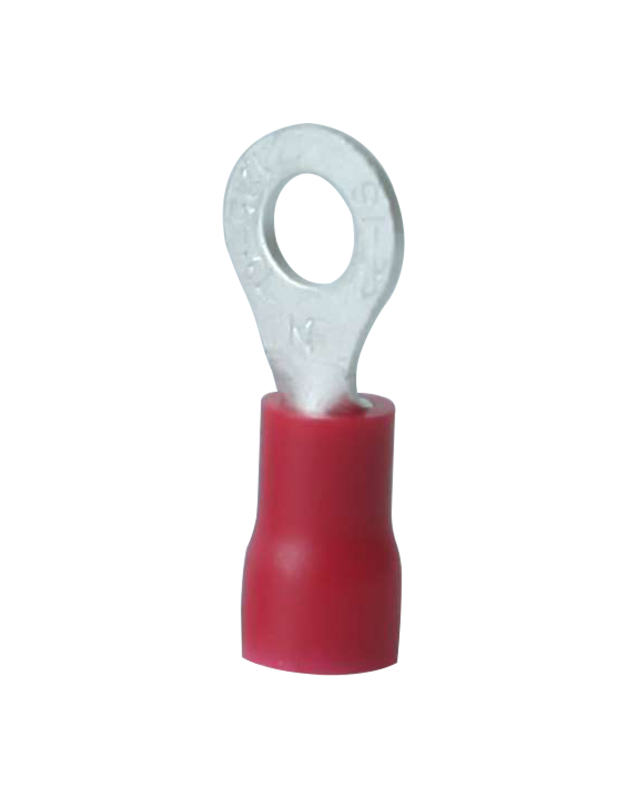
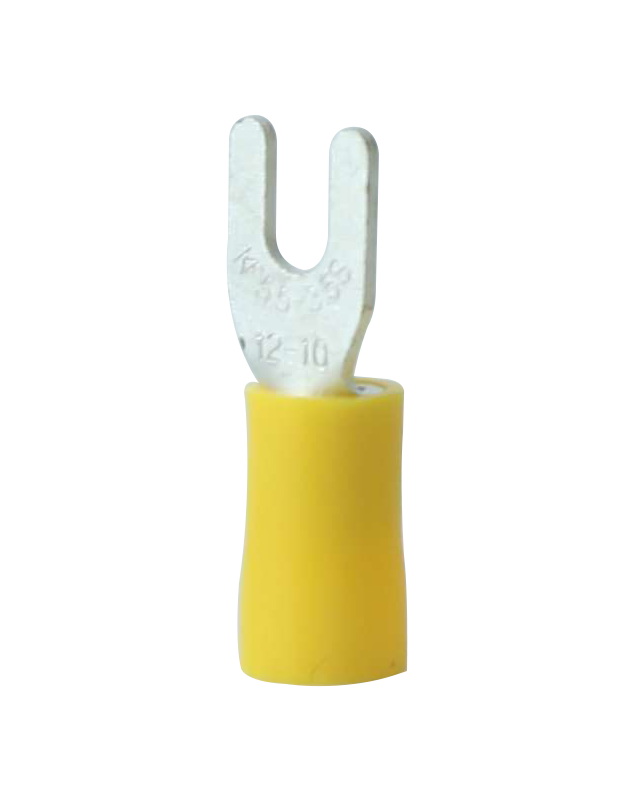
Figure 5 — Same manufacturer, same insulation material, two colours and two terminal shapes. The collar colour marks a conductor range within that manufacturer’s own range; the shape is a separate choice. Treat the colour as a production aid, not as the specification.
The colour code is a production aid. Once the size has been decided from the wire range, the colour lets an operator pick up the right part quickly and lets an inspector confirm it at a glance. Selection runs in the other direction: identify the conductor, check its class, then read the terminal’s published range — and treat the collar colour as confirmation that the correct part was picked up, not as the specification itself.
The same caution applies to ferrule collars. The colour band on a cord end ferrule is a size marker tied to a manufacturer’s own range, not a universal standard, and it should never be the basis for matching one brand’s part against another’s.
Can AWG be converted to mm² exactly?
No. AWG is defined by conductor diameter on a logarithmic scale and mm² by cross-sectional area. The two were standardised independently, so an exact conversion always falls between the metric sizes. Use the conversion to interpret a drawing, then select against the terminal’s published wire range.
Is 16 AWG the same as 1.5 mm²?
No. 16 AWG has an actual cross-section of 1.31 mm². 1.5 mm² is the nearest standard size in the IEC 60228 sequence, but it is a different conductor. Select the terminal against its published range rather than against a rounded metric label.
Is 14 AWG the same as 2.0 mm²?
No. 14 AWG measures 2.08 mm², and 2.0 mm² is not part of the IEC 60228 standard sequence at all. The nearest standard size is 2.5 mm². Where a terminal range is stated as 1.5–2.5 mm², a 14 AWG conductor falls inside it.
Does a larger AWG number mean a thicker wire?
No. The AWG scale runs backwards: a higher number means a thinner conductor, so 18 AWG is thinner than 12 AWG.
Why do two cables marked 2.5 mm² look different?
Because of conductor class. At 2.5 mm², a Class 1 solid conductor is a single 1.78 mm wire and a Class 2 conductor is typically 7 strands of 0.67 mm, while a Class 5 conductor may use around 50 strands and a Class 6 around 140. The copper area matches; the construction does not.
Should I round a conductor down to fit a smaller terminal?
Never. Rounding down forces the strands to deform and reduces the contact area of the crimp. Choose the terminal whose published range contains the conductor.
What exactly does a terminal’s wire range mean?
It is the minimum and maximum conductor size that the barrel will accept and crimp correctly. The conductor has to fall inside that window; a terminal that almost fits will not produce a reliable joint.
Does insulation colour tell me the size?
Not reliably. Colour conventions differ between manufacturers and between regions. Identify the conductor first, then confirm the terminal against its published wire range.
Can I use the same crimping tool on AWG and mm² terminals?
The tool has to match the barrel, not the measurement system. Check the tool and die recommended for the specific terminal part number; KF lists a tool against each size in the Type AWG range.
Does a data sheet always list both AWG and mm²?
Not always. Where only one system appears, convert the conductor using the table above and confirm the result against the range that is published. On a mixed-system project, fix one system as the drawing reference.
Send us the conductor size and class, the terminal type and the application. We will confirm the matching part number and its published wire range from the product data sheet. Drawings and technical support are available on request.
References: ASTM B258, standard specification for AWG sizes of solid round copper wire; IEC 60228, conductors of insulated cables. Conversion values are calculated from the AWG defining formula and are provided to help interpret drawings — always confirm the wire range published for the specific terminal part number.
You can tick the products you need and communicate with us in the message board.


Allen.Mo


Jackie.Li


Jasmine.Zhang


Roy.Liu